A Common Confusion in Production Planning
Manufacturing organisations frequently use the terms constrained resource and bottleneck resource as though they were interchangeable. They are not. The distinction becomes critical when companies begin exploring advanced production scheduling, optimisation algorithms, or detailed planning tools.
Understanding the difference determines whether sophisticated scheduling methods will actually help or merely create complicated plans that no one can execute.
Identifying Constrained Resources
A practical way to identify constrained resources is to examine utilisation levels over time. If a machine, work centre, or human resource consistently operates above roughly eighty percent utilisation across several months, it can reasonably be considered constrained.
At this point the organisation is operating near the limits of available capacity. Demand begins to compete for the same production slots, and planners must carefully sequence operations to avoid missed delivery dates. This is typically the moment when companies begin talking about optimisation techniques and advanced scheduling tools.
By contrast, when resource utilisation remains significantly lower, sophisticated optimisation rarely produces meaningful value. If utilisation remains below roughly two thirds of available capacity, traditional planning methods such as material requirements planning often remain sufficient.
In simple terms, a constrained resource indicates that available capacity is struggling to keep up with immediate demand.
The Moving Nature of Bottlenecks
Bottlenecks are different. A bottleneck is whatever slows the flow of work through the system at a particular moment. Unlike constrained resources, bottlenecks are rarely permanent. They move as production conditions change.
Unexpected downtime, inefficient staffing patterns, missing materials, or poor job sequencing can temporarily transform an otherwise normal resource into a bottleneck. Once the situation resolves, the bottleneck may appear somewhere else in the process.
Because bottlenecks move, identifying them reliably through static analysis is difficult. Many experienced planners rely on observation of production queues and operational behaviour rather than purely analytical identification.
Scheduling Heuristics and Bottlenecks
Advanced planning systems often include scheduling heuristics designed to handle bottleneck resources. For example, certain SAP scheduling rules deliberately prioritise operations that pass through designated bottleneck work centres. The intention is to protect the flow of work through the most critical parts of the process.
However, the results of such heuristics are rarely straightforward. Prioritising one resource can delay operations elsewhere in the system. Orders may start later than planned, due dates may shift, or other resources may sit idle waiting for the bottleneck to clear.
This is why scheduling outcomes frequently require human interpretation. The software can generate schedules, but the planner must evaluate the economic consequences of those schedules.
Limits on Bottleneck Designation
Some planning systems allow multiple resources to be designated as bottlenecks, though doing so excessively defeats the purpose of the concept. In practice only a small fraction of resources should be classified this way. If too many work centres are labelled as bottlenecks, the scheduling logic loses its ability to prioritise effectively.
The designation should therefore remain limited and deliberate.
When Bottlenecks Are Not Constrained
An interesting situation can occur when a resource behaves like a bottleneck even though it is not technically constrained. Consider a workstation that occasionally slows production because of operator behaviour, inconsistent staffing, or irregular material supply. The resource itself may possess sufficient capacity on paper, yet operational inefficiencies cause queues to form in front of it.
In such cases the bottleneck arises from operational behaviour rather than structural capacity limits.
A Practical Analogy
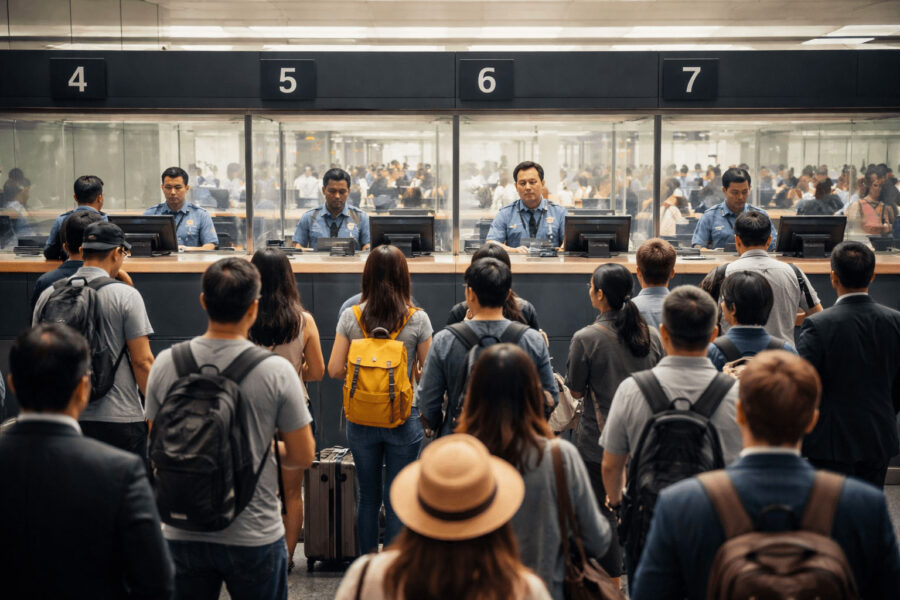
A familiar analogy can be found in airport immigration lines. The immigration counter itself may not be constrained by design. Several counters may exist, and the physical infrastructure may support high throughput. Yet if one officer works slowly or repeatedly leaves the desk, queues can quickly build at that counter.
The system appears constrained from the traveller’s perspective, but the underlying issue lies in operational behaviour rather than physical capacity.
The Planner’s Responsibility
Ultimately, production scheduling is not merely a mathematical exercise. A capable production manager understands the economic consequences of scheduling decisions. Every delayed order carries a financial implication. Every unnecessary prioritisation may disrupt another order with higher business value.
Experienced planners therefore focus on the economic risk associated with scheduling outcomes. They evaluate which orders carry significant consequences if delayed and which can safely move within the schedule.
This practical judgement often matters more than the specific heuristic used by the planning system.
The Real Lesson
Before organisations invest heavily in advanced scheduling projects, they should ensure that both consultants and internal teams understand the operational realities behind these concepts. Sophisticated optimisation tools are useful only when planners understand the business consequences of the schedules they produce.
In production scheduling, software can calculate possibilities. It remains the responsibility of people to decide which outcomes actually make sense for the business.