The Question Every Planner Eventually Asks
Supply chain planning systems present a long list of lot sizing options. Fixed lot sizes, lot-for-lot replenishment, minimum batch quantities, economic lot sizes, and time-based lot sizing rules such as n-day supply. For someone implementing material requirements planning, the number of choices can appear overwhelming.
The natural instinct is to search for the “correct” formula.
In practice, the correct answer rarely comes from a formula alone.
The Limits of Textbook Lot Sizing
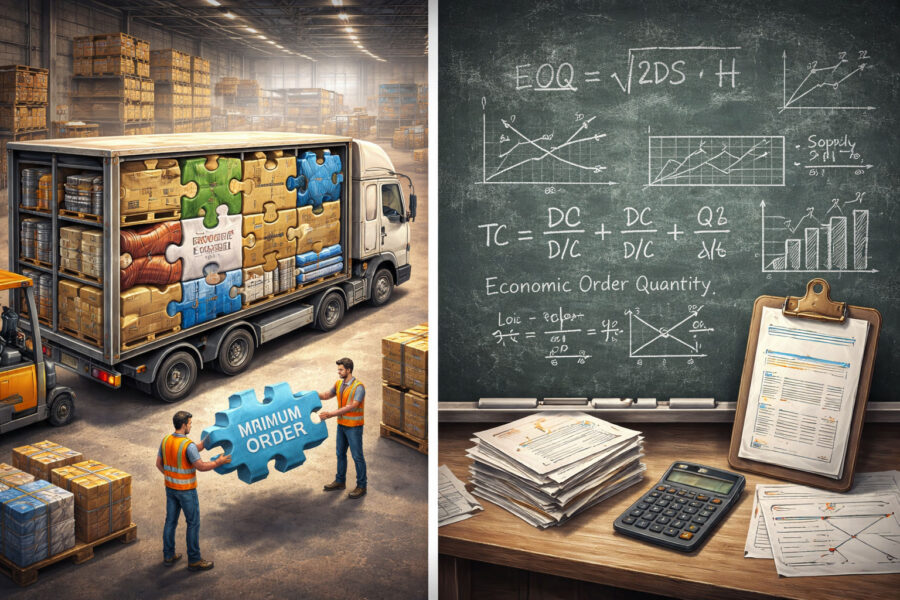
Classic supply chain theory offers mathematical approaches such as economic order quantity or batching rules designed to balance inventory holding costs against ordering costs. These models assume relatively stable conditions and well-defined cost structures.
Real supply chains rarely operate under such clean assumptions.
Companies deal with supplier constraints, transportation economics, packaging limitations, contractual obligations, production batch sizes, and fluctuating demand patterns. Each of these factors influences the practical size of supply orders.
Lot sizing therefore becomes less about mathematical optimisation and more about aligning planning parameters with business reality.
When Fixed Lot Sizes Make Sense
In some cases the appropriate lot size is obvious because it is determined by the physical production process. If a manufacturing line produces cheese in blocks of ten kilograms, the planner cannot realistically order nine kilograms or seventeen kilograms.
In such situations the lot size simply reflects the production unit itself.
Similarly, certain production environments operate with fixed batch sizes because of equipment constraints or process requirements. In these cases setting a fixed lot size in the planning system mirrors how production actually works.
When Simplicity Works Better
For lower-value items the planning approach may be much simpler. Many inexpensive components are managed effectively through reorder point planning or maximum stock limits. When inventory drops below a threshold, replenishment is triggered automatically.
This method avoids unnecessary complexity and works well for items with stable consumption patterns and relatively low financial impact.
However, even inexpensive components can occasionally carry high operational importance. A low-cost fastener may become critical if its absence halts production of a high-value product.
The economic context therefore always matters.
The Complexity of Multi-Product Supply Chains
Lot sizing becomes even more complicated when suppliers deliver multiple products together or when manufacturers ship mixed loads to distribution centres. In these environments the economics of transportation and handling often dominate individual product planning parameters.
A supplier may prefer shipping consolidated loads rather than responding to precise quantities calculated separately for each product. Transportation capacity, pallet configuration, and shipping frequency influence what actually arrives at the warehouse.
These commercial realities often override textbook lot sizing rules.
The Forecast Splitting Debate
Another common planning idea involves splitting forecasts into smaller time buckets. Planners sometimes assume that moving from weekly forecasts to daily forecasts will automatically create more precise supply plans.
In practice this assumption does not always hold.
Lot sizing rules and batching constraints can interact with smaller forecast buckets in unexpected ways. Minor demand fluctuations may trigger additional production orders or purchase orders that increase work-in-progress inventory and create unnecessary volatility.
Greater detail does not always produce better planning outcomes.
Vendor Constraints and Minimum Quantities
Many supply chains operate under vendor-imposed purchasing constraints. Suppliers may require minimum order quantities or shipment thresholds that must be met regardless of calculated demand.
In such cases planners sometimes adjust order quantities across multiple products to reach the required threshold. The objective becomes filling a shipment economically rather than following strict lot sizing rules for each individual item.
This behaviour resembles the early stages of the well-known bullwhip effect, where small demand changes propagate through the supply chain as larger order fluctuations.
Commerce Before Theory
These examples illustrate a broader truth about supply chain planning. Business rules and commercial realities typically shape planning behaviour more strongly than theoretical models.
Transportation economics, vendor agreements, storage capacity, production processes, and demand volatility all influence how replenishment decisions are made.
Planning parameters should therefore reflect these realities rather than blindly following textbook formulas.
The Practical Principle
When implementing basic supply chain planning systems, organisations benefit from beginning with their business constraints. Once the commercial drivers are understood, theoretical models can be used to refine planning parameters.
Theory helps calibrate the system. It rarely defines the entire solution.
In supply chain planning, mathematics provides useful guidance. The final answer usually emerges from the economics of the business itself.